Engineering · Olive oil mills
Olive pomace, dealt with at the mill
Every campaign ends the same way: wet, acidic tonnes you pay to have taken away, on a waste tax that stands at 40 € a tonne in 2026 and is legislated to reach 60 € by 2030. A pyrolysis unit at the mill turns most of that mass into water vapour and biochar, and the disposal liability into a carbon removal in your own name.
This page is the honest version. Pomace is the hard case: the unit's own recovered heat goes into drying it, so the value is residue treatment and carbon, not energy. We would rather tell you that in the first paragraph than in a footnote.
The arithmetic
What your pomace becomes
Fresh pomace is roughly two-thirds water, so every honest figure below is a fraction of the dry third, not of what leaves your decanter. Biochar comes out at 25–32% of dry matter, and each tonne of it holds 1.7–2.1 tonnes of CO₂e, a touch below the woody range, because pomace char carries more ash.
The panel shows a 2,000-tonne campaign, run through the same factors as the estimator on our engineering page, including a permanence factor of 0.80 for Portuguese soil temperatures, not the Nordic figure. These are design estimates: the assessment measures your actual material.
Indicative: 2,000 t of fresh pomace
- Biochar produced
- 180–220 t
- Durable CO₂ removed
- 300–470 tCO₂e
- Recoverable heat
- Self-consumed in drying
- Residue mass removed
- ~1,800 t
25–32% of dry matter: a stable, carbon-rich char.
Durable for several centuries (CORC200+), net of lifecycle emissions.
Evaporating the water consumes the unit's own recovered heat. On pomace, energy is not the case.
Mass in, minus biochar out: the number your disposal budget cares about.
How it works
A unit that runs on the worst residue you have
01
Receive & dry
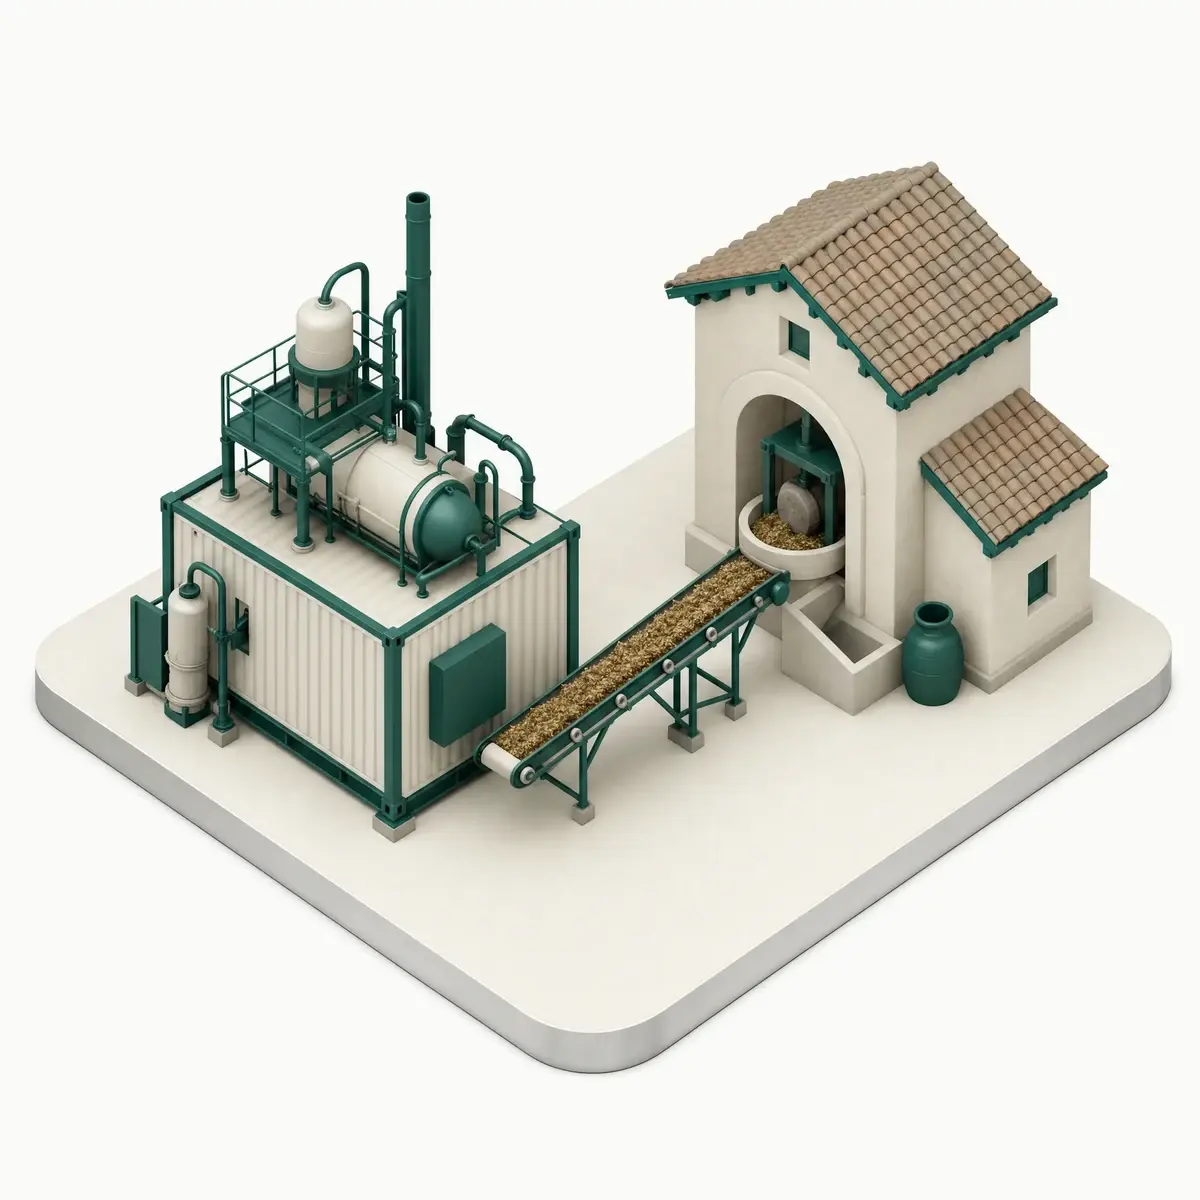
Pomace arrives as it leaves your process. The unit's recovered heat drives a dryer that brings the moisture down until the material can sustain pyrolysis; this is where the energy goes, by design.
02
Pyrolyse
The dried pomace is heated without oxygen. Instead of burning, it decomposes: gas is drawn off and burned to power the process, and the carbon skeleton remains as biochar.
03
Collect
Biochar discharges into big bags: a dry, stable material at around a tenth of the mass you started with. The rest left as water vapour and process gas, not on a lorry.
04
Record
Every batch is logged as it happens (feedstock in, char out, samples to the laboratory), so the removal can be certified rather than merely claimed.
Two ways to own it
Buy the unit, or buy the outcome
Equipment supply
You own the unit
We design, deliver and commission a unit sized to your campaign, train your team and stay on for support. The capital investment is yours, and so are the biochar, the heat balance and the carbon.
Your capex · your operation · full upside
Build-Own-Operate Agreement
We run it at your mill
No capital outlay: we finance, build, own and operate the unit at your site, and you pay per tonne of pomace processed. Your benchmark is what disposal costs you today, a figure already legislated to rise. The outputs are still yours.
No capex · per-tonne fee · you keep the outputs
Keeping the removal inside your own footprint is insetting, and the vocabulary (offsetting, insetting, durability) is defined in plain terms in the glossary.
The carbon story
A removal your olive oil can claim
Pomace biochar locks its carbon away for several centuries (the CORC200+ durability class). That removal can go one of two ways: certified and sold as carbon credits, or kept inside your own footprint (insetting), so the olive oil you bottle carries a measured removal from its own residue. One or the other, never both.
Built into every unit
- Feedstock intake records (origin, mass, moisture) captured digitally at the mill.
- Batch-level data and accredited laboratory analysis, mapped to the EBC and registry methodologies.
- The removal counted in your olive oil's footprint, or certified as credits. Your choice, evidenced either way.
Where we stand: our first industrial facility is in development, first production is planned for 2027, and no client units have shipped yet. Engineering assessments are open now, and early clients set the queue.
Size it for your tonnes
The estimator on our engineering page runs the arithmetic above against your own volume, pre-set to fresh pomace, and honest about the heat.
Open the estimatorFAQ
What mill owners ask us
Six questions we hear from mills, including the one about whether this is worth doing at all.
How an assessment works
Four steps, no fee to find out
01
One call
Residue type, rough tonnes per year, moisture and season, what you do with heat today. Thirty minutes.
02
Site visit
We sample the material and walk the space, access and connections with you.
03
The assessment
A written design estimate: unit envelope, biochar output, exportable heat, mass reduction, CO₂e. Figures you can hold us to.
04
Your decision
Buy the unit, or we build and run it at your site. Either way, the carbon stays yours.
Tell us about your pomace
Tonnes per campaign, what you do with it today, and where the mill is: the assessment starts there, and it costs you nothing.
Request an assessment